Case study · A cable and aluminum-coil plant in China
12-ton coils moved with ±10 mm docking.
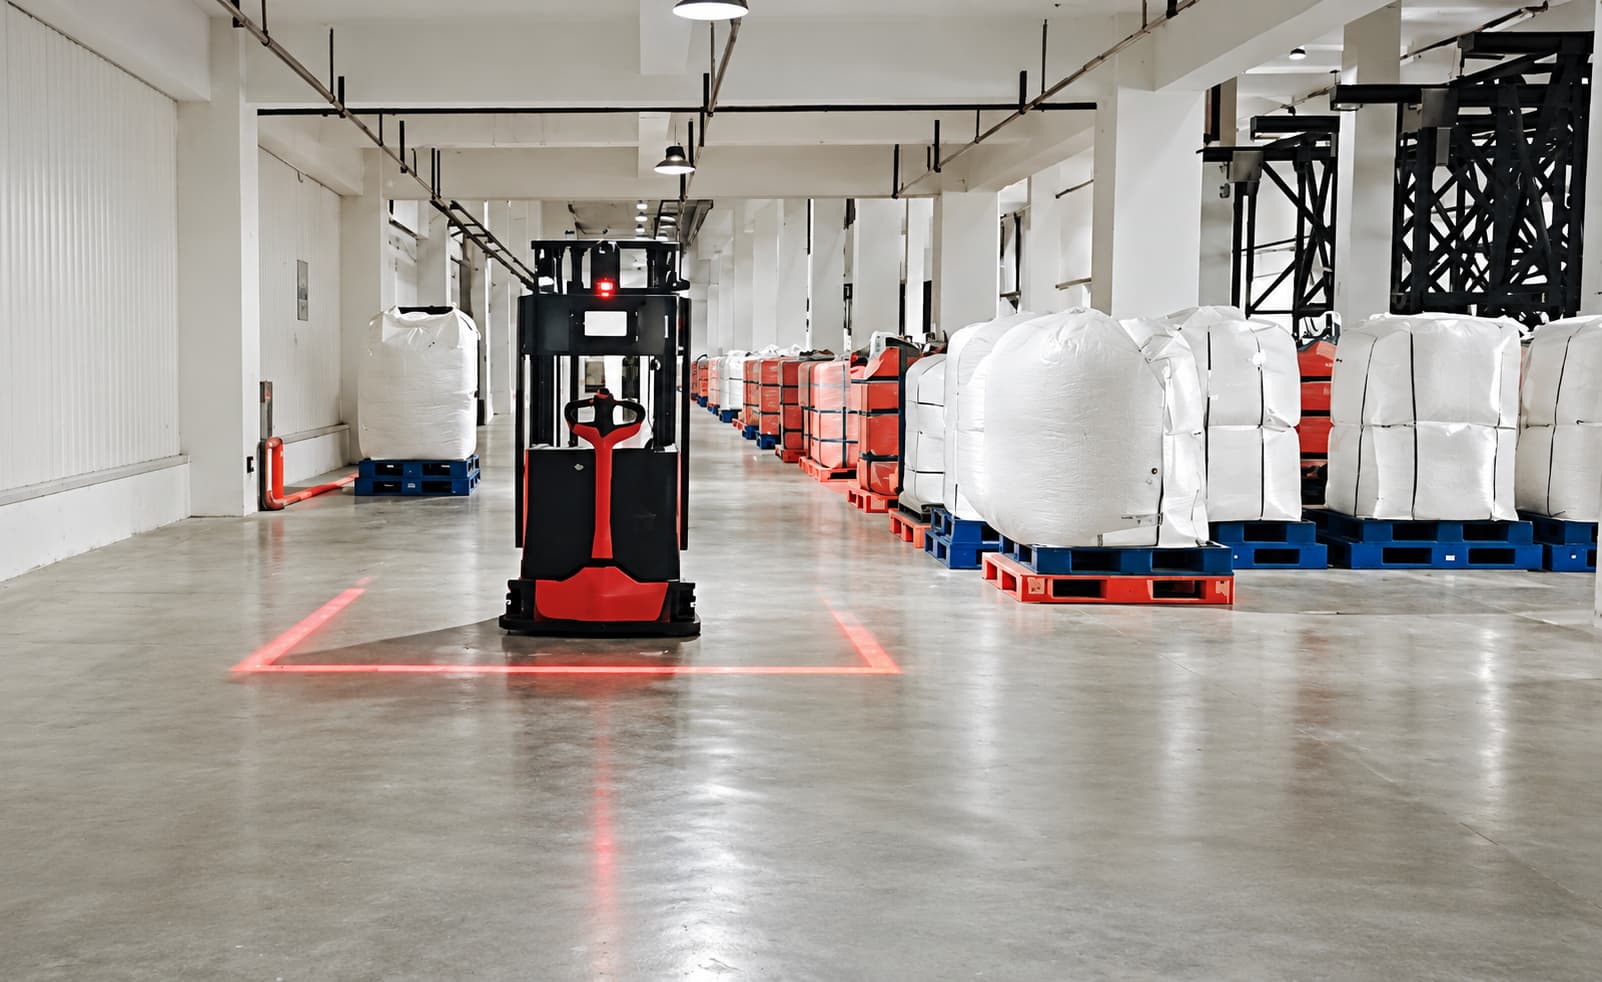
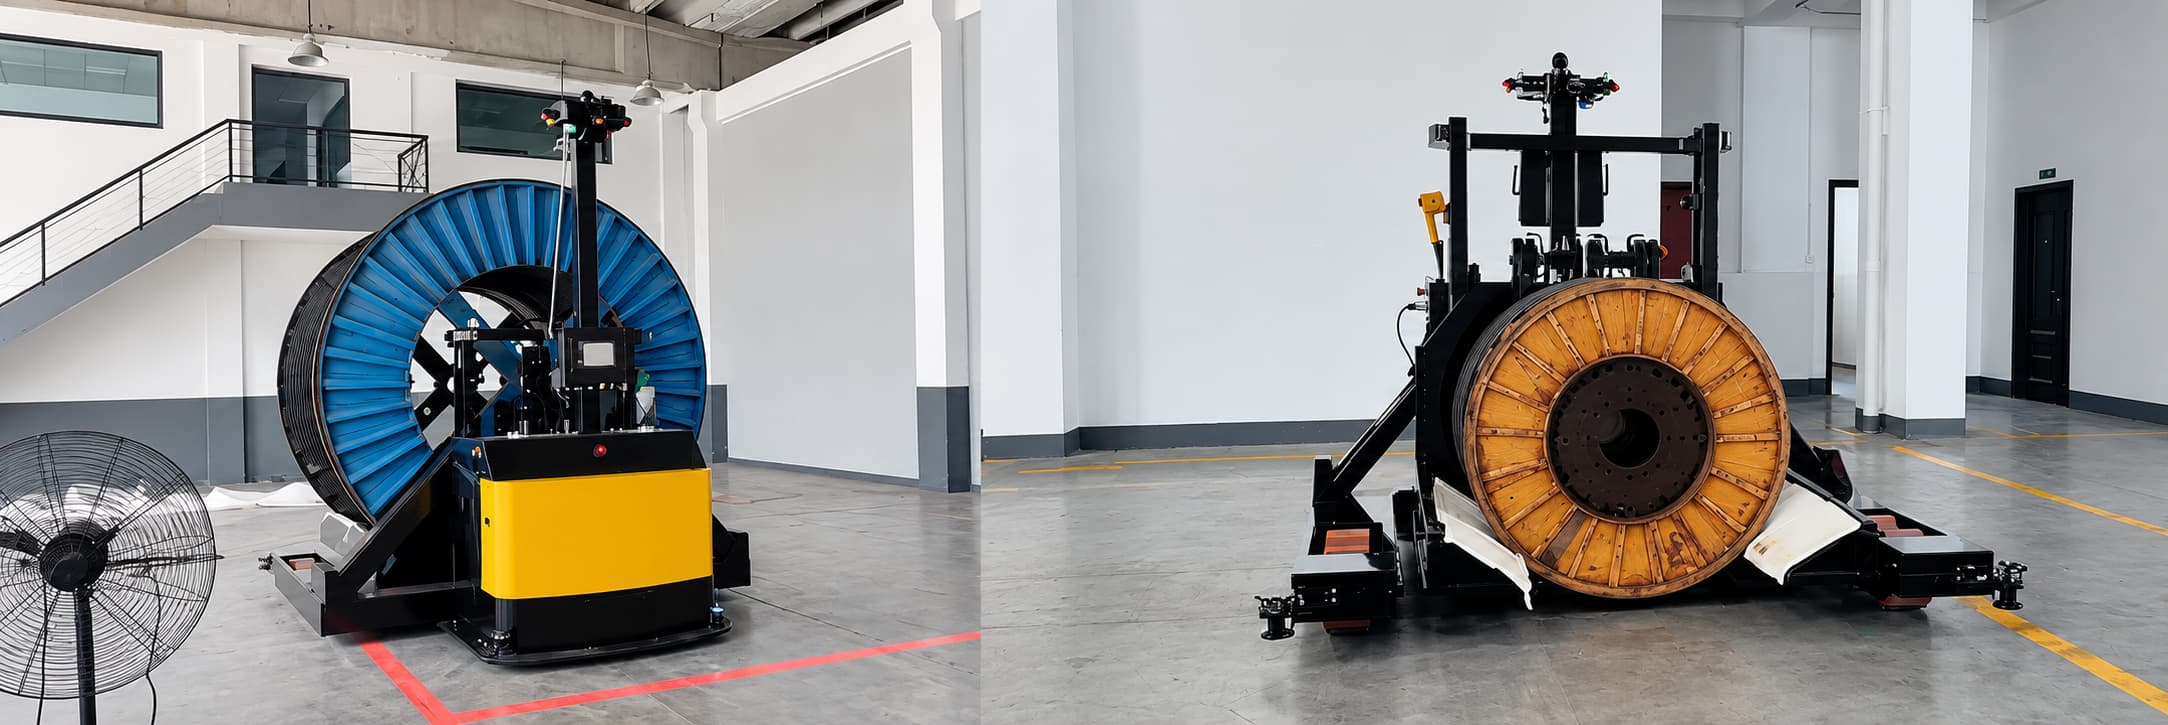
A custom forklift AMR now connects coil drop-off, cache, machine feeding, leftover return and outbound movement while keeping heavy reels stable in transfer.
12 t
Maximum coil payload
±10 mm
Pickup and docking accuracy
Near-zero
Coil damage in transfer
Figures reported by the manufacturing partner. Product category: Autonomous forklifts
At a glance
The plant needed one flow for 12-ton aluminum coils and finished cable reels. A purpose-built forklift AMR with ramped forks now handles the full route and docks at ±10 mm, keeping transfer damage near zero.
About the plant
This is a cable and aluminum-coil plant in China. The operation moves heavy aluminum coils and finished cable reels between production, cache and outbound staging. The material is cylindrical, smooth and difficult to pick with a standard forklift.
The challenge
A single coil can weigh more than 10 tons. Manual forklift runs connected four steps that did not share one schedule: line-end drop-off, feeding the drawing machines, leftover return, and finished-reel outbound.
- Heavy coils had to leave the line quickly without blocking aisles.
- Drawing machines needed coils on takt, not when a driver became available.
- Leftover coils varied in size and were easy to mis-record on return.
- Finished reels were equally heavy, so outbound loading stayed slow and exposed to collision risk.
The solution
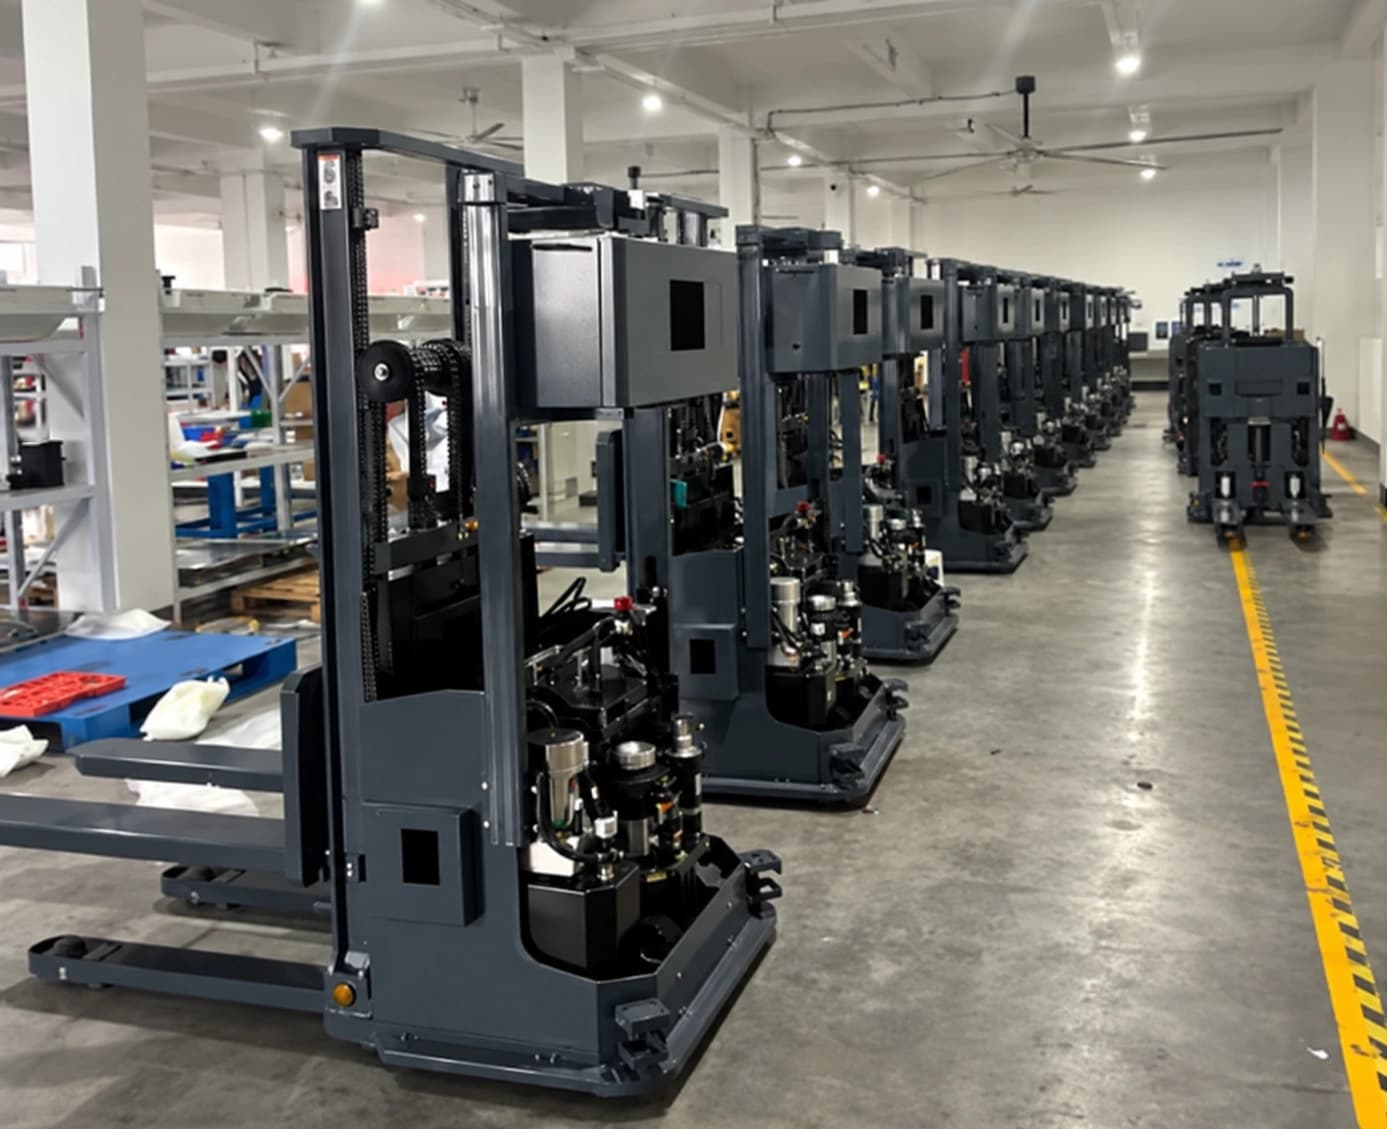
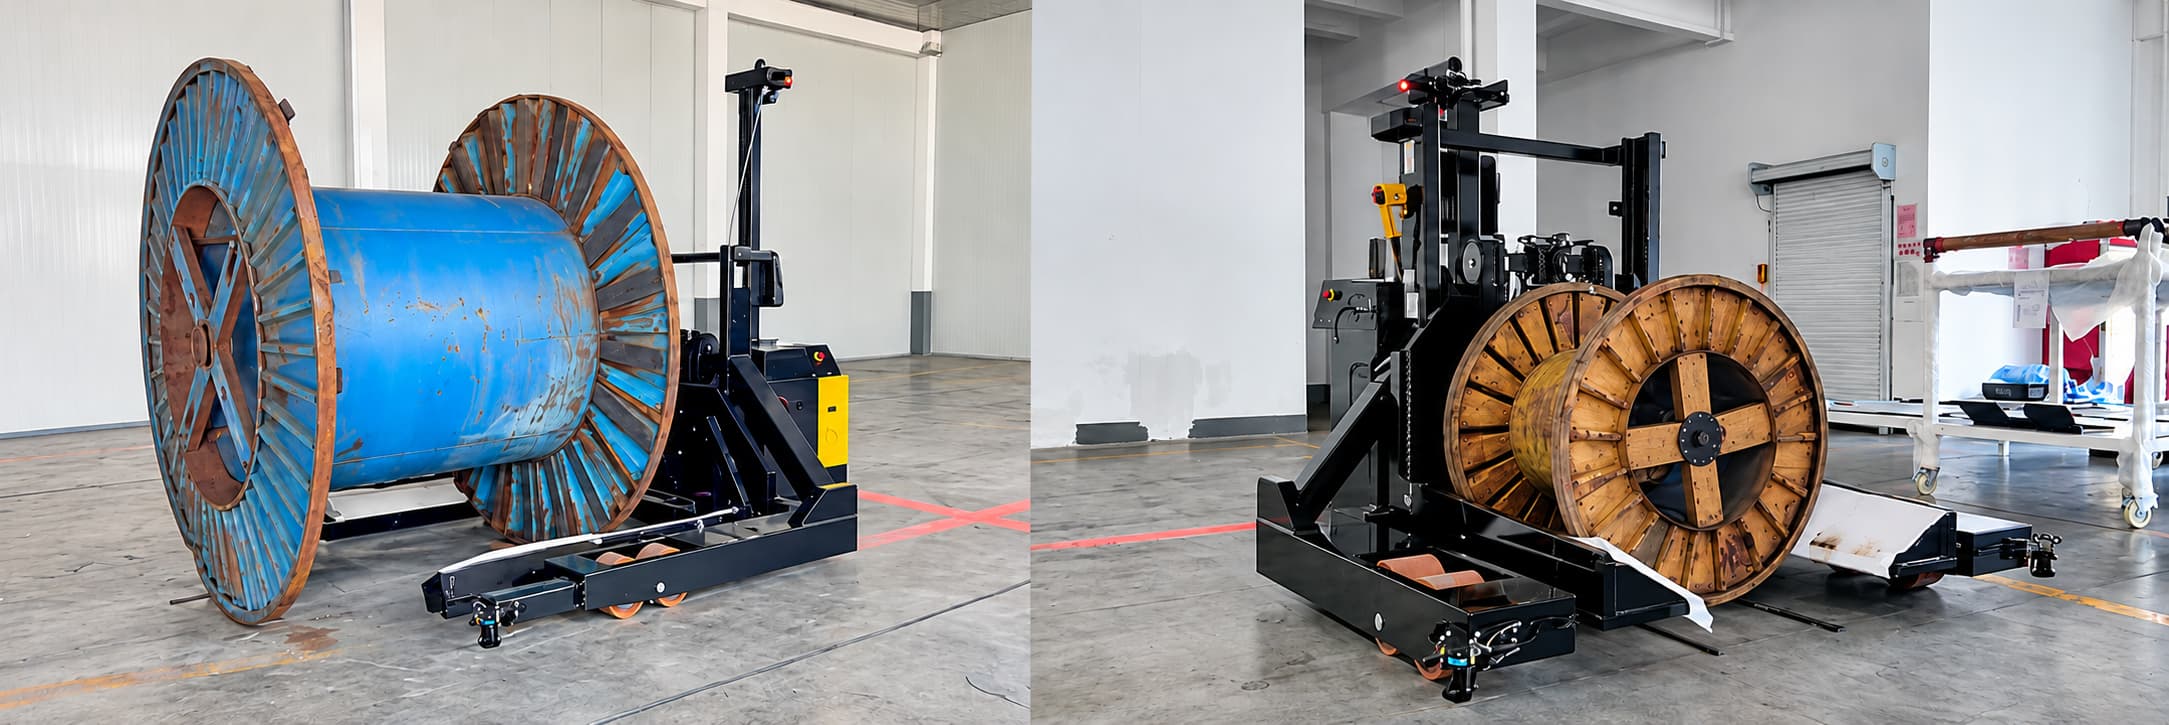
The plant deployed a custom heavy-duty forklift AMR built around the coil geometry. Ramped forks follow the inner arc of the reel so the load sits instead of rolling. Solid tires keep the vehicle stable on shop-floor slopes.
Laser navigation maps the plant without magnetic tape. Vision at the fork tips finds the coil and the machine dock, then finishes the last move to ±10 mm. The same vehicle now covers line-end, cache, machine feeding, leftover return and outbound.
The result
The connected flow shortened coil movement from line-end to machine, return and outbound. Forklift operators moved off repetitive coil transfers. Transfer damage dropped to near zero, and each coil, leftover reel and finished reel now keeps a location record through the route.
- One automated flow handles coils up to 12 tons.
- Visual docking reaches ±10 mm at pickup and machine-feed points.
- Controlled handling keeps transfer damage near zero.
Plan a similar plant flow.
Share the payload, route and docking points. BotOnly will map the work to a short list of systems that can run the same class of plant job.